Does used machine come with export customs clearance documents?
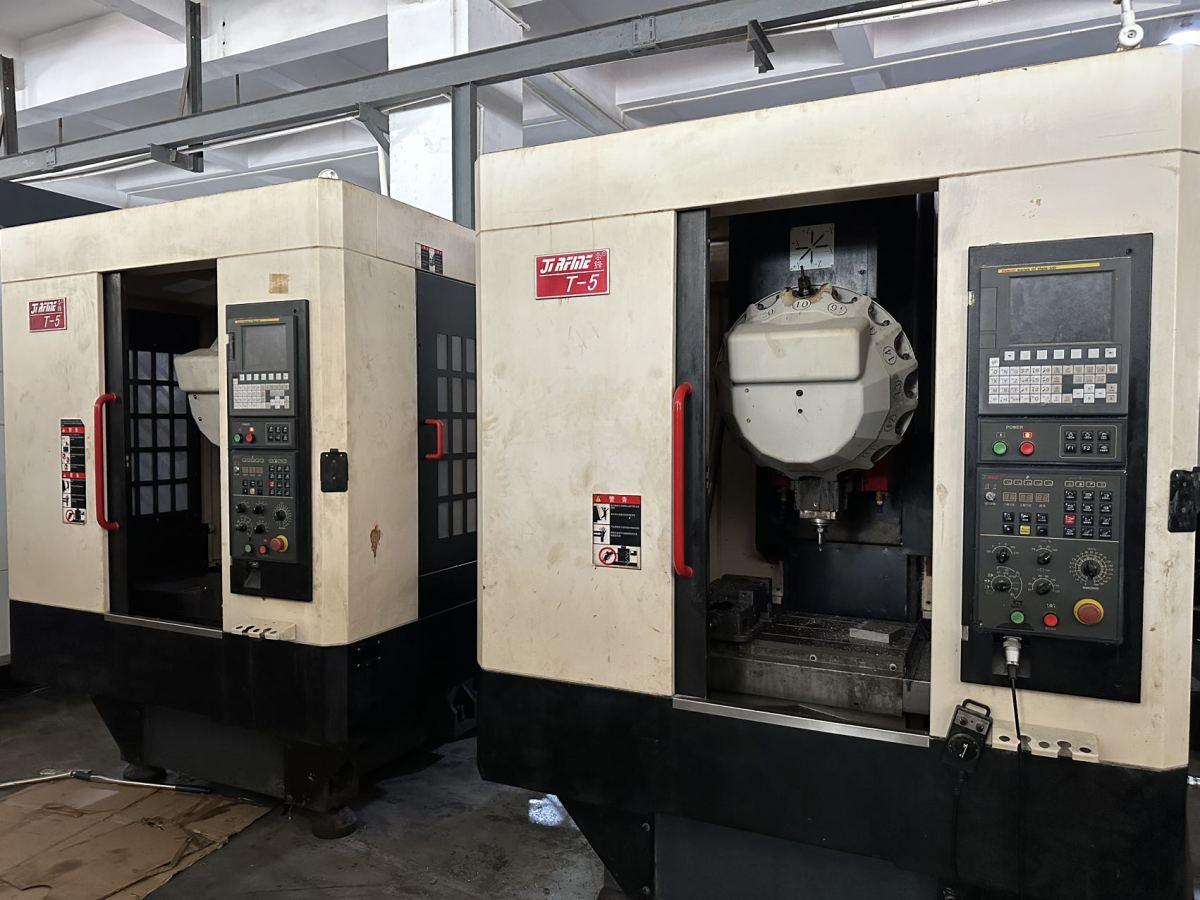
When sourcing affordable and functional second-hand industrial and construction machines overseas, most international buyers have a core concern: does a used machine come with complete export customs clearance documents? This question directly determines whether your shipment can pass customs smoothly, avoid penalties, and complete import procedures successfully. In this guide, we answer this question in detail and share key knowledge for safe used machine import trade.
Official Answer: Qualified Used Machines Include Standard Export Documents
Genuine and legally exported used machines from professional trading companies always come with full export customs clearance documents. Only personal sellers, unregistered small merchants, and informal private transactions fail to provide official customs files.
Different from new machinery, used machines are subject to stricter inspection and supervision in global cross-border trade. Customs authorities worldwide strictly check the legality, usage status, safety and environmental compliance of second-hand equipment to prevent obsolete, unqualified or polluting machines from entering local markets. Therefore, formal export documents are a mandatory standard for legitimate used machine export.
Complete Customs Clearance Document List for Used Machines
Reliable suppliers will prepare a full set of standard documents before shipment to support global customs clearance.
First, the commercial invoice records the machine’s brand, model, production year, serial number, technical parameters, transaction price and trade terms, serving as the core basis for customs tax calculation and cargo verification.
Second, the formal export customs declaration form is the most critical document. It proves that the used machine has completed official customs filing, passed official review and meets national export standards without trade restrictions.
Third, a detailed packing list marks the machine’s weight, size, packaging information and supporting accessories, ensuring consistency between declared information and physical goods.
In addition, certificate of origin, bill of lading and equipment inspection reports are provided as standard attachments. For engineering, mechanical and electrical used machines, professional safety and quarantine certificates will also be offered to prove compliance with international import standards.
Risks of Purchasing Machines Without Export Clearance Documents
Buying used machines without complete customs documents will bring huge trade risks. Customs departments in all countries will detain undocumented cargo, resulting in long-term shipment delays.
In most cases, buyers will face high customs fines, cargo return costs and additional storage fees. Worse still, unrecorded and undocumented used machines cannot be registered, used or resold legally in the local market, causing serious economic losses to your business.
How to Get Fully Documented Used Machines for Export
To ensure a risk-free transaction, you must cooperate with formal, licensed used machinery export suppliers. Before placing orders, confirm the complete document list with suppliers and verify the validity of customs declaration files.
Professional suppliers can also adjust document contents according to the customs policies of different countries, ensuring fast and barrier-free import clearance for every used machine shipment.
Conclusion
In short, formal exported used machines definitely come with complete export customs clearance documents. Complete paperwork is the basic guarantee of legal trade, safe logistics and normal equipment use. Always prioritize documented and compliant used machines to protect your international trade interests.
More Articles
-
Used CNC Machine Inspection Checklist: 10 Things to Check Before BuyingA used CNC machine inspection should establish whether the machine can produce your parts reliably and what repairs the purchase may require. Clean paint and a smooth demonstration do not prove accuracy. Before testing, agree on acceptance criteria based on your workpiece tolerances, machining process and installation requirements. Confirm the machine’s identity and configuration Match the nameplate model and serial number to the quotation and records. Confirm the CNC control version, axis configuration, installed options, electrical requirements and included accessories. Request operating hours where available, but treat them as context: counters may have been reset or replaced. Used CNC machine inspection: 10 actionable checks Check Action and expected evidence 1. Structure and crash damage Inspect castings, table, covers and spindle area for cracks, impact marks or repairs. Photograph suspect areas. 2. Spindle condition Run through agreed speeds after warm-up; note noise, vibration and temperature trends. Measure runout using suitable calibrated equipment. 3. Guideways and lubrication Inspect accessible ways, seals and lubrication delivery. Check for scoring, corrosion, damaged covers and dry surfaces. 4. Axis motion Traverse each axis through safe usable travel at different feeds. Check reversal behavior, abnormal noise, servo loads and alarms. 5. Tool magazine and changer Where fitted, cycle multiple pockets repeatedly with suitable toolholders. Check indexing, retention and transfer consistency. 6. CNC control and electronics Test startup, display, keys and program transfer. Review alarm history, backup availability and enabled options. 7. Positioning and geometry Request positioning, repeatability and relevant geometry measurements, with methods, instruments and test conditions recorded. 8. Cutting performance Run an agreed representative test cut. Measure critical dimensions and finish; record material, tooling and cutting conditions. 9. Auxiliary systems and safety Test coolant, chip removal, hydraulics or pneumatics, emergency stops and interlocks. Record leaks and faults; never bypass safeguards. 10. Maintenance and repairs Review dated service records, replaced components and supporting invoices. Match major repairs to subsequent test results. Turn test evidence into purchase conditions Record results against the machine’s serial number, including warm-up state, instruments and acceptance limits. A test cut validates only the conditions tested; positioning and geometry checks help identify errors it may miss. For unresolved faults, obtain repair estimates and require a repeat test where performance is affected. Put included equipment, acceptance conditions and responsibility for dismantling, loading and transport into the purchase agreement. Plan leveling and verification after installation. Buyer questions before committing How should accuracy be verified? Use calibrated measurements and a representative test cut against agreed part requirements. Display resolution alone does not establish machining accuracy. What if maintenance records are missing? Treat condition as less certain. Expand independent inspection and price the unresolved repair risk before committing. Can remote inspection replace an onsite visit? Live video can screen candidates. Request continuous footage showing machine identity, startup, movements and measurements; use an independent onsite inspector for critical checks. Which warning signs justify pausing? Refused testing, unexplained alarms, inconsistent identification, structural cracks or unsupported accuracy claims warrant investigation before payment.

-
CNC Machining Center Buying Guide: How to Choose the Right Machine for Your BusinessThe right CNC machining center must handle your parts, meet drawing requirements and support your production schedule within an affordable total cost. This CNC Machining Center Buying Guide follows that decision sequence: define the work, select the configuration, verify specifications and compare complete purchase proposals. Start with representative parts and production targets Prepare drawings covering your largest workpiece, hardest material and most demanding features. Record material grades, finished dimensions, tolerances, surface finish, batch sizes and annual demand. Include fixture dimensions and weight: a part that fits the table may still lack adequate tool access. Set a realistic cycle-time target that includes loading, tool changes, probing and inspection. For mixed production, setup time and programming effort can matter as much as cutting speed. Match the machine type to the work A vertical machining center is often a practical starting point for general milling, plates and accessible components. A horizontal machining center warrants consideration for repeated machining on multiple faces, particularly when pallet handling and chip evacuation support the production plan. Consider five-axis capability when complex geometry or fewer setups justify the programming, workholding and verification requirements. Distinguish indexed positioning from simultaneous five-axis cutting; the required toolpaths determine which capability you need. Verify specifications against the complete setup Requirement Relevant parameter Buyer verification Part and fixture fit Axis travel, table load, spindle clearance Check the complete setup and tool approach throughout travel. Material removal Spindle torque, power, speed range Match the torque curve to intended tools and cutting conditions. Drawing compliance Positioning accuracy, repeatability, thermal behavior Agree on a representative cutting and measurement procedure. Production continuity Tool capacity, coolant, chip removal Allow for required tools, sister tools and material-specific chips. Maximum spindle speed alone does not establish productivity. Check controller functions, CAM postprocessor compatibility and any required software licenses before committing. Build the budget and purchase checklist together Compare total installed cost, including freight, rigging, utilities, tooling, fixtures, software, commissioning and training. Then assess maintenance, consumables, service access and likely downtime. Request an itemized quotation identifying included options and exclusions. Confirm floor loading, access dimensions, electrical supply and compressed-air requirements. For used equipment, review service records and arrange checks of spindle condition, axis motion, lubrication and tool changing. Document acceptance criteria, delivery responsibilities and agreed support terms in writing. Buyer FAQ What should take priority when the budget is limited? Protect work-envelope fit, cutting capability and required accuracy first. Defer optional automation if current volumes do not justify it, while checking whether later upgrades are feasible. How can buyers compare different machine proposals fairly? Give each supplier the same drawings, materials, batch assumptions and acceptance requirements. Compare the proposed process, complete configuration and installed cost on that shared basis.

-
What to Consider When Buying a Boring Machine from a ManufacturerA boring machine manufacturer should be evaluated against your repair or production task—not simply its catalog range. Before requesting a quotation, provide workpiece drawings, bore dimensions, material, access restrictions, required geometry and finish, and expected duty cycle. For portable line boring, include mounting locations and site power. These details let you assess whether the supplier can engineer a workable solution rather than merely quote a machine. Check who controls engineering and production Ask which activities the supplier performs directly: design, machining, assembly, control integration and final testing. Outsourcing is not automatically a weakness; unclear responsibility is. A credible industrial boring machine supplier should identify who controls critical components, supplier qualification and corrective action. Request a live factory walkthrough or an independent audit covering machines comparable to your proposed configuration. General workshop footage does not establish application competence. Ask an engineer to explain the proposed setup, tooling reach, support arrangement and limitations. Manufacturer Evaluation Checklist Area Evidence to request Risk to resolve Engineering Application review and proposed configuration Unverified assumptions about access, rigidity or tooling Production control Process responsibilities and critical-component records Uncontrolled substitutions or unclear accountability Quality control Inspection plan, calibration records and sample reports Claims unsupported by measurement Machine testing Agreed cutting test and acceptance report No-load demonstration mistaken for machining proof Lifecycle support Parts list, warranty terms and service procedure Downtime without a clear recovery route Make acceptance measurable before ordering Agree on factory acceptance testing before paying a deposit. Define the test material, tooling, setup, cutting conditions, measurements and pass/fail criteria. A spindle-running video cannot demonstrate bore accuracy or surface finish under load. For a boring machine factory, quality evidence should connect component inspection, assembly checks and final testing to the delivered machine. Specify who witnesses testing, which records accompany shipment, and how failures are corrected and retested. Where site conditions affect results, distinguish factory acceptance from commissioning checks. Verify customization and post-delivery responsibility For custom configurations or OEM/ODM projects, document design ownership, branding, drawing approval, software access and change control. Confirm whether modifications affect parts availability or service documentation. Request written warranty coverage, exclusions, claim procedures and responsibility for labor, travel and freight. Verify spare-part identification, quoted availability, remote troubleshooting and commissioning arrangements. For exports, clarify packing, shipping documents, destination compliance responsibilities and manuals; export capability alone does not establish suitability for your country. Supplier audit and procurement FAQ Is a factory visit essential? Not always. A live remote audit, independent inspection and witnessed cutting test can reduce risk. Higher-value or heavily customized projects justify deeper verification. How should competing manufacturers be compared? Issue the same application brief and acceptance requirements. Compare documented technical fit, exclusions and support obligations—not headline price or claimed factory size.

-
Boring Machine Maintenance Guide: How to Keep Equipment Running ReliablyReliable boring machine maintenance starts with controlling contamination, friction, cutting forces and alignment errors before they become downtime. A practical maintenance program should follow the machine’s operating conditions and manufacturer instructions rather than rely on one fixed service interval. Before inspection or cleaning, isolate power and secure moving components according to the applicable safety procedure. Cleanliness and lubrication protect moving components Chips, abrasive dust and coolant residue can enter slideways, bearings, gearboxes and electrical enclosures. This contamination increases friction and can cause sticking, accelerated wear or overheating. Remove chips with suitable tools, wipe exposed surfaces, and keep slideways, feed screws, spindle areas and clamping surfaces free from debris. Do not direct high pressure air toward bearings, seals or control cabinets. Check lubrication points, oil levels and grease condition against the machine manual. Confirm that lubricant reaches the intended bearing, slideway or gear. Excess lubricant can attract abrasive material, while insufficient lubricant increases temperature and wear. Inspect for leaks and identify the source before simply adding more lubricant. Inspect tools, boring bars and alignment A damaged insert or dull cutter increases cutting force and may produce vibration, poor surface finish and oversize bores. Check inserts, holders and tool clamping before each job. Replace damaged cutting edges and verify that the tool is seated securely. Record recurring edge damage because it may indicate excessive load, poor chip evacuation or incorrect cutting conditions. The boring bar is especially sensitive to deflection, runout and unsupported length. Inspect the bar for scoring, bending, damaged threads and worn mounting surfaces. Clean the bar, holder and spindle interface before assembly. If the machine shows taper, chatter or inconsistent bore size, check tool runout, workpiece clamping and machine alignment before changing cutting parameters. Check the drive, motor and electrical system Abnormal noise, heat, vibration, odor or unstable speed can indicate problems in the motor, drive, bearings or power connections. Keep cooling paths clear and inspect accessible cables, connectors, switches and protective devices for damage or looseness. Electrical enclosure filters and fans should remain clean so heat can escape. When an alarm, repeated trip or irregular motion occurs, stop the machine and record the operating condition, alarm code and recent maintenance work. Qualified personnel should test electrical components and determine whether the cause is mechanical resistance, a control fault or a power issue. Maintenance checklist and spare parts planning Maintenance Item Recommended Check Cleaning Remove chips, dust and coolant residue from slides, tooling, guards and work areas. Lubrication Verify lubricant level, delivery and leakage using the machine manual. Tooling and boring bar Check inserts, runout, mounting surfaces, deflection and clamping security. Motor and electrical system Inspect cooling, cables, connectors, alarms, vibration and abnormal temperature. Storage Clean, dry and protect exposed machined surfaces; release or secure components as specified. For long-term storage, clean and dry the machine, apply the specified corrosion protection, cover it in a dry ventilated area and follow the manufacturer’s instructions for batteries, lubricants and movable axes. Keep commonly replaced inserts, seals, filters, fuses and other model-specific items identified by part number. Confirm compatibility before ordering; the correct spare part depends on the machine version and assembly. FAQ How often should a boring machine be maintained? Use operating hours, load, environment, coolant exposure and manufacturer guidance to set inspection intervals. Cleaning and visual checks may be needed more frequently in abrasive or high-chip environments. What should be checked when bore accuracy changes? Inspect the tool edge, boring bar runout, clamping, spindle condition, lubrication and machine alignment. Check one factor at a time and document the result. Which spare parts should be kept available? Identify wear items and failure-prone components from the machine manual and service history. Verify part numbers, revisions and interchangeability with the equipment supplier before purchase.